Carbon steel
Coating selection must balance corrosion exposure, appearance, edge protection, part geometry and dimensional tolerance.
- Powder coating
- Wet spray painting
- Electro-galvanizing
- Hot-dip galvanizing
- Phosphating
- Black oxide

Powder coating, painting and corrosion protection
In-house automated powder coating for light parts and a dedicated painting shop for large or heavy fabrications, supported by finish selection for steel, stainless steel and aluminium.
One fabricated-part supplier, one finish specification
Surface treatment is not a cosmetic afterthought. The correct system depends on the base metal, outdoor exposure, expected service life, part geometry, coating thickness, colour, electrical contact requirements and acceptable appearance.
Fabex can fabricate, prepare and finish complete sheet metal parts. Our in-house powder and wet-paint capabilities reduce handoffs for common enclosures and assemblies. For processes such as hot-dip galvanizing, electro-galvanizing, anodizing, passivation and PVD, we coordinate the approved specialist process with the fabrication requirements.
Tell us the environment and performance requirement, not only a colour. We can flag water traps, thin edge coverage, masked areas, galvanic pairs and dimensional changes before they become field corrosion or assembly problems.

Start with the substrate
These are practical starting points. The drawing and purchase specification should define the final process, thickness, appearance and validation requirements.
Coating selection must balance corrosion exposure, appearance, edge protection, part geometry and dimensional tolerance.
Finishing is normally selected for appearance, cleanability or restoration of the passive corrosion-resistant surface.
Anodizing, conversion coating and paint systems can provide appearance, adhesion, weather resistance or wear performance.
| Material | Treatment | Typical build | Common use | Engineering considerations |
|---|---|---|---|---|
| Carbon steel | Powder coating | Typically 60-120 µm | Cabinets, power boxes, equipment housings and fabricated assemblies | Durable and economical with broad colour and texture options. Cure heat, recess coverage, threads, fits and cut edges need review. |
| Carbon steel | Wet spray paint | Typically 20-50 µm | Large or heavy parts, smooth decorative finishes and high-gloss colour requirements | More flexible for large fabrications and fine appearance, but usually less scratch resistant than powder and requires VOC/process control. |
| Carbon steel | Electro-galvanizing | Typically 5-15 µm | Internal brackets, fasteners and concealed structural parts | Low dimensional change and several passivation colours. Thin zinc is not the first choice for long-term exposed outdoor service. |
| Carbon steel | Hot-dip galvanizing | Often 40-80 µm; standard-dependent | Outdoor baseplates, shelving structures, guards and heavy-duty steelwork | Strong long-term corrosion protection, with a rougher appearance and greater risk of distortion, drainage marks and dimensional change. |
| Carbon steel | Phosphate or silane pretreatment | Conversion layer | Preparation before powder coating or wet paint | Improves adhesion and corrosion performance but is normally not specified as the final exposed finish. |
| Carbon steel | Black oxide | Minimal dimensional change | Internal, non-cosmetic components | Provides a matte black appearance but limited rust resistance. Oil or another seal is required. |
| Stainless steel | Brushing, polishing or sandblasting | Mechanical finish | Visible panels, appliance parts, enclosures and architectural components | Grain direction, acceptable weld blending and cosmetic surface class should be defined on the drawing. |
| Stainless steel | Passivation | Chemical treatment | Parts requiring a clean passive surface after fabrication or welding | Usually creates no visible colour change. Specify the required standard and any cleanliness or testing requirement. |
| Aluminium | Anodizing | Class and thickness by specification | Decorative panels, wear surfaces and outdoor aluminium parts | Natural, coloured and hard-anodized options are available. Anodizing is electrically insulating, so contact and grounding areas may need masking. |
| Aluminium | Powder coat, wet paint or conversion coat | System-dependent | Large coloured housings or parts requiring a paint-bonding pretreatment | Alloy, pretreatment, exterior exposure, colour, gloss and electrical contact requirements determine the correct system. |
Typical thicknesses are planning ranges, not acceptance criteria. Final values depend on the material, process standard, coating system and approved project specification.
Outdoor applications
Material, pretreatment, coating, drainage, edges, seams and maintenance all influence service life. A thicker topcoat cannot compensate for poor preparation or water-trapping geometry.
Specify the exposure
Indoor dry, sheltered outdoor, direct rain, coastal salt, industrial pollution, UV, chemicals and design life lead to different finish choices.
Consider hot-dip galvanizing for robust sacrificial zinc protection. A duplex system, galvanizing plus a compatible topcoat, can add colour and extend service life.
Review: Review vent and drain holes, enclosed cavities, welds, threads, fit-up allowances, appearance expectations and distortion risk before release.
A suitable pretreatment followed by exterior-grade powder coating is a common route. Projects may specify a 100-120 µm film build where geometry and coating-system guidance allow.
Review: Define ingress exposure, coastal or industrial atmosphere, colour/gloss, coating system, masking, grounding points, gasket lands and required test standard.
Protection must cover the complete assembly, not only broad flat faces. Zinc-rich cut-edge touch-up, seam sealing or a revised coating sequence can be specified where appropriate.
Review: Sharp edges naturally receive less film build. Edge radiusing, weld finishing, drainage and avoiding water traps improve real-world corrosion performance.
Controlled finishing workflow
The standard preparation flow for sprayed carbon-steel parts is degreasing, rinsing, rust removal where needed, phosphating or silane treatment, drying, coating and cure.
We review the substrate, service environment, drawings, colour, gloss, film build, cosmetic class and compliance requirements.
Parts follow the approved sequence for degreasing, rinsing, rust or oxide removal, conversion treatment and drying.
Light parts run through our in-house automated powder line; large and heavy parts use our painting shop. Specialist treatments are coordinated to the approved specification.
The finish is cured or completed to its process requirements, then checked for coverage, appearance, colour, film build and protected features.
Finished surfaces are separated and packed to reduce rubbing, impact, contamination and cosmetic damage in international transport.

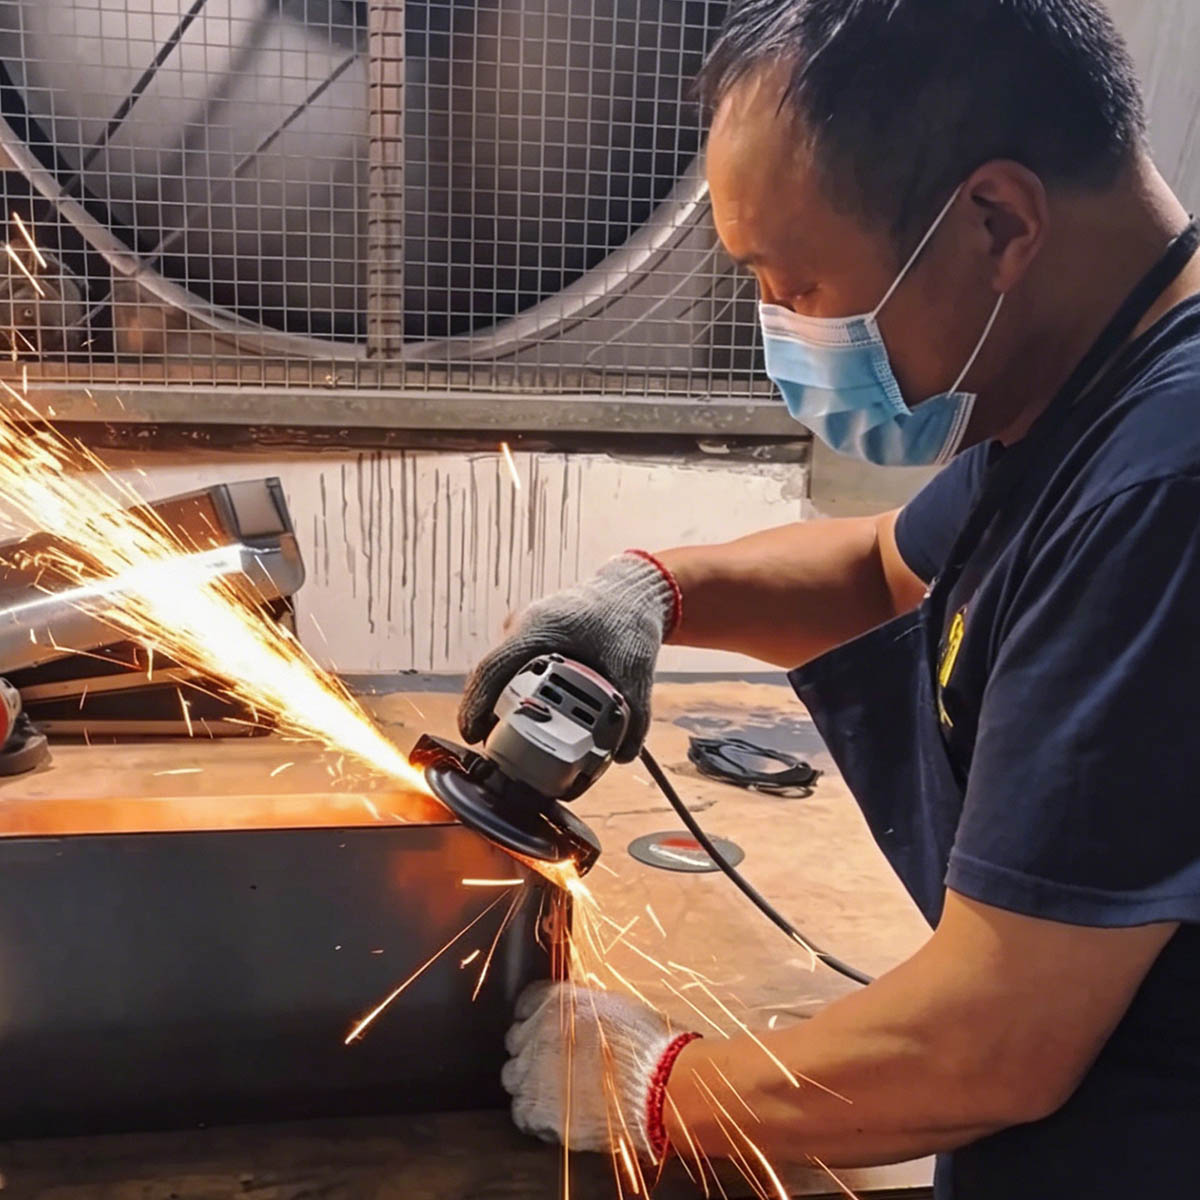
Large or heavy part?
Send the part envelope and weight with the RFQ. We will confirm handling, preparation, booth access, cure or drying route and packaging before quoting.
Discuss part size and finishInspection plan
A finish can look acceptable and still fail at threads, gasket interfaces or exposed edges. We convert the drawing and purchase requirements into practical inspection points before production.
RFQ checklist
Finish-aware DFM
Finish performance depends on geometry and fabrication details as much as the coating name. Fits, edges, seams and drainage need review before production.
View the complete sheet metal DFM guideFor powder coat, typical c = 0.06-0.12 mm per surface; an opening may reduce by approximately 2c.
Identify threads, grounding points, gasket lands, bearing fits and cosmetic faces that require masking.
Provide practical hanging and drainage features for wet processes, and avoid sealed pockets or water traps.
Technical questions
Answers to the finish questions that most often affect quotation, corrosion performance and assembly.
In sheet-metal purchasing, "electrostatic painting" commonly refers to electrostatic powder coating: charged powder adheres to the grounded part and is then oven cured. Electrostatic equipment can also apply liquid coatings, so the drawing or purchase specification should still state powder or liquid paint explicitly.
Yes, a 100-120 µm target can be reviewed for suitable parts and coating systems. We confirm the powder supplier guidance, part geometry, cure schedule, critical fits, thread masking and inspection locations before accepting it as a controlled requirement.
There is no single answer for every outdoor environment. Hot-dip galvanizing is often suitable for heavy structural steel, while properly pretreated exterior-grade powder coating is common for enclosures. Coastal, high-UV, chemically exposed or long-design-life applications may require a duplex or project-specific system.
We review edge sharpness, weld condition, pretreatment access, drainage and the complete coating sequence. Depending on the specified system, the solution may include edge radiusing, weld dressing, zinc-rich touch-up, seam sealing or increased attention to film-build inspection at vulnerable areas.
Fabex supplies fabricated parts with brushing, polishing, passivation, anodizing, blasting and related finishes. Processes outside our in-house powder and painting facilities are managed through the approved finishing workflow. State the required standard, appearance, masking and test records in the RFQ.
Send the drawing, material, quantity, part size and weight, finish specification, colour/gloss/texture, service environment, cosmetic surfaces, masking details and any film-thickness or corrosion-test requirement. A photo or physical reference is useful when appearance is critical.
Send your drawings, service environment and finish requirement. Fabex will review fabrication details, anti-rust risks and the practical coating route with your quote.